How to Choose the Best Hot Melt Roller Coating Machine?
Choosing the right Hot Melt Roller Coating Machine is not simply a matter of comparing prices or motor power. The real decision depends on adhesive viscosity, coating width, substrate behavior, production speed, and temperature control. A machine that performs beautifully with EVA adhesive may struggle with pressure-sensitive formulations. Small differences matter.
Adhesive technology specialist Dr. Robert W. Tess offers a useful principle: “The adhesive must be selected for the process, not merely for the product.” This idea should guide every equipment comparison. Check the roller’s heating uniformity, gap adjustment, pump compatibility, cleaning access, and control response. Ask for coating samples using your actual material. Factory demonstrations can reveal defects that brochures never mention.
Look closely at the production floor. Is the hot melt reservoir easy to refill? Can operators remove residue without wasting hours? Does the machine maintain a stable coating line when speed changes? These practical details influence quality, maintenance costs, and worker confidence. Energy consumption also deserves attention, especially during long shifts.
There is no universally perfect machine. That assumption causes expensive mistakes. A compact model may suit narrow web production, while a wider industrial system may justify its higher investment. Still, specifications alone are insufficient. Review service support, spare-part availability, safety features, and documented test results before purchasing. The best Hot Melt Roller Coating Machine is the one that delivers consistent coverage under your real operating conditions, not merely impressive performance in a showroom.
Understand How Hot Melt Roller Coating Machines Work
How to Choose the Best Hot Melt Roller Coating Machine?
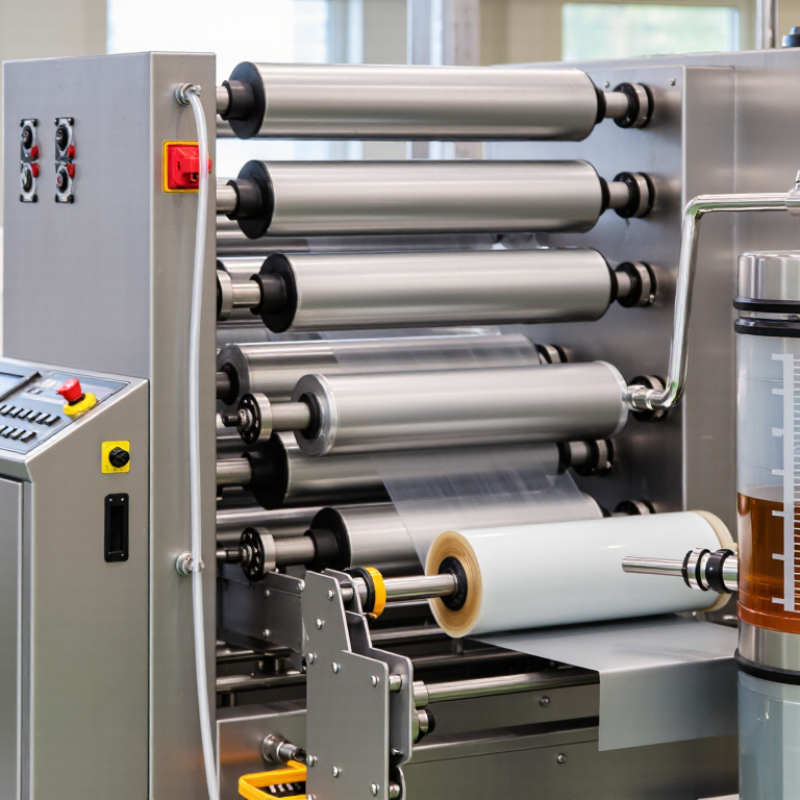
A hot melt roller coating machine turns solid adhesive into a controlled liquid film. Heated tanks or hoses melt the material before application. A pump then moves it toward the coating rollers. The applicator roller transfers adhesive onto the substrate, while a metering roller controls thickness. Roller speed, temperature, pressure, and gap work together. Small changes can affect coat weight, edge quality, and bonding strength. A warmer setting is not always better. Excessive heat may damage the adhesive or substrate.
When choosing equipment, match the machine with your material and production speed. Check its working temperature range, roller width, coating tolerance, and cleaning access. Operators should also examine how quickly the system reaches a stable temperature. Uneven heating can create thin lines, bubbles, or unwanted buildup. In real production, these faults often appear after several hours, not during a short test. Request practical trial data, maintenance instructions, and measurable performance limits. Do not rely only on attractive specifications.
Tips: Start with a small coating trial. Record temperature, line speed, roller gap, and adhesive weight. Inspect the coating under steady lighting. Test adhesion after cooling, not immediately. Keep a sample from each trial for comparison. It is easy to blame the machine first, but moisture, surface dust, or incorrect substrate tension may be responsible. This part deserves honest review.
Define Your Coating Material and Production Requirements
Choosing the best hot melt roller coating machine starts with the coating material, not the machine catalog. Identify its melting range, viscosity, open time, tack, and solid content. These properties control roller temperature, gap settings, pump load, and coating stability. A material that flows well at 120°C may become stringy at 150°C.
Check the substrate carefully. Film, foam, paper, and fabric absorb or reject adhesive differently. Record the substrate width, surface energy, thickness, and heat tolerance. Also define the target coating weight, line speed, coating width, and daily operating hours. Small details matter. A trial at 20 grams per square meter may fail when production reaches 60 meters per minute. I have seen this mistake create uneven edges and wasted rolls.
Production requirements should guide the machine’s working range. Choose a roller system that can maintain steady temperature and pressure during long runs. Ask whether it supports the required coating pattern, quick material changes, and practical cleaning access. Confirm electrical capacity, ventilation, operator protection, and routine maintenance needs before purchase. Do not rely only on supplier calculations. Test the actual material with the actual substrate whenever possible. The first estimate is often wrong. A short pilot run can reveal buildup, poor bonding, or unstable coating weight before these problems reach full production.
Evaluate Speed, Precision, Safety, and Maintenance Features
Choosing a hot melt roller coating machine starts with the production target, not the catalog speed. A faster roller can reduce cycle time, but unstable temperature control may create streaks, edge buildup, or uneven coating weight. I would compare usable output at the required width, not the maximum speed on the specification sheet. Test samples at low, medium, and peak speeds. Measure coating weight, web tension, and temperature variation. Precision matters most.
Small errors become expensive.
Deloitte’s 2024 Global Smart Manufacturing Survey found that 86% of manufacturers expect smart manufacturing to become a major competitiveness factor within five years. Therefore, select equipment that records temperature, pressure, speed, and alarm history. These records support process improvement and help technicians find recurring faults. Safety deserves equal attention. The U.S. Bureau of Labor Statistics reported about 2.6 million nonfatal workplace injuries and illnesses in private industry during 2023. Look for guarded rollers, emergency stops, insulated hot surfaces, and clear lockout procedures. Maintenance access should not require awkward reaching near heated components. Check nozzle cleaning, roller removal, spare-part availability, and lubrication intervals before purchase. Preventive maintenance is useful, but it is not magic. Operators still need practical training and visual inspection routines. A short factory trial may reveal more than a polished brochure.
How to Choose the Best Hot Melt Roller Coating Machine? - Evaluate Speed, Precision, Safety, and Maintenance Features
The following comparison uses typical operating ranges for industrial hot melt roller coating systems. Actual performance depends on adhesive chemistry, substrate, coating width, coating weight, and production conditions.
| Machine Configuration | Typical Line Speed | Coating-Weight Range | Coating-Weight Accuracy | Temperature Control | Roll Gap Adjustment | Safety Features | Routine Maintenance | Overall Suitability Score | Best Application |
| Laboratory or Pilot-Scale Roller Coater | 1–20 m/min | 10–200 g/m² | Typically ±5–10% | Usually ±2–3°C | Manual micrometer or handwheel adjustment | Basic guarding, emergency stop, heated-surface warning | Frequent roller cleaning; manual adhesive charging and inspection | 3/5 | Product development and small batches |
| Standard Single-Roller Coating Line | 10–60 m/min | 15–250 g/m² | Typically ±3–7% | Usually ±1–2°C | Manual or motorized gap control | Safety guards, emergency stops, over-temperature protection | Daily roll cleaning and weekly inspection of seals, bearings, and heaters | 4/5 | General-purpose converting |
| Precision Metering Roller Coater | 20–100 m/min | 5–150 g/m² | Typically ±2–5% | Usually ±1°C | Motorized adjustment with digital position feedback | Interlocked guarding, emergency stops, pressure and temperature alarms | Scheduled calibration, roll parallelism checks, filter and seal replacement | 5/5 | Consistent technical coatings |
| Wide-Web Industrial Roller Coater | 30–150 m/min | 15–300 g/m² | Typically ±3–6% | Usually ±1–2°C across heated zones | Automatic or synchronized motorized adjustment | Full guarding, interlocked access doors, emergency-stop circuits, web-break protection | Planned shutdown cleaning, automatic lubrication where available, alignment checks | 5/5 | High-volume web processing |
| Compact Modular Hot Melt Coater | 5–50 m/min | 10–200 g/m² | Typically ±3–8% | Usually ±1–3°C | Quick-change manual or servo-assisted adjustment | Thermal insulation, emergency stop, guarding around nip and drive areas | Accessible melt-path cleaning and quick replacement of wear components | 4/5 | Flexible production with frequent changeovers |
| Selection guidance: Prioritize speed and web handling for high-volume production; prioritize roll-gap control and temperature stability when coating-weight consistency is critical; verify guarding, interlocks, emergency stops, over-temperature protection, cleaning access, spare-part availability, and preventive-maintenance requirements before purchase. |
Select a Machine That Fits Your Budget and Future Capacity
How to Choose the Best Hot Melt Roller Coating Machine?
A suitable hot melt roller coating machine should match today’s budget without limiting tomorrow’s production. Begin with your actual coating width, adhesive type, working temperature, and daily running hours. A low-cost model may look attractive, but slow heating or uneven roller pressure can increase waste and labor costs. Ask for a coating trial using your material, not a standard sample.
Calculate the complete investment. Include electrical installation, ventilation, spare rollers, cleaning tools, operator training, and routine maintenance. Check how quickly the tank reaches temperature and whether controls show stable readings. Small details matter. A machine that saves ten minutes during every changeover may repay its higher price over time. However, buying excessive capacity can leave expensive equipment idle.
Plan for realistic growth. Choose adjustable line speed, replaceable rollers, and enough heating capacity for your expected next stage. If production may double, confirm that the frame, drive system, and power supply can support future upgrades. Speak with technicians who can explain maintenance intervals and common failure points. Their answers should be specific, not merely confident. I would also keep a written cost comparison for three years, because initial estimates are often too optimistic. Leave room for error. A practical choice is usually the machine your team can operate consistently, maintain safely, and expand without rebuilding the entire line.